
Steel vs. Stainless Steel CNC Machining: Differences in Cost, Tooling, and Tolerance
When selecting materials for CNC-machined parts, the choice might appear—based solely on the technical drawings—to be a matter of corrosion resistance. From the perspective of the machine shop floor, however, it is fundamentally a question of machinability. Compared to similar carbon steels, stainless steels are more prone to work hardening during machining, exhibit greater heat accumulation in the cutting zone, and cause more rapid tool wear. These factors influence production cycle times, tooling costs, and final surface quality—all of which are reflected in the quotes you receive for your Request for Quotation (RFQ), leading to variations in the per-unit price.
This guide compares these two categories of materials across several key factors that affect machining costs and part quality: cutting speed, tool life, thermal properties, tolerances, and surface finish. It focuses on some of the most common grades used in machining: carbon steels (1018, 1045, and 4140) and stainless steels (303, 304, 316, and 17-4 PH). The data provided represent typical ranges encountered in a production environment; actual values may vary depending on factors such as heat treatment condition, cutting tool geometry, machine tool rigidity, and the application of coolant.
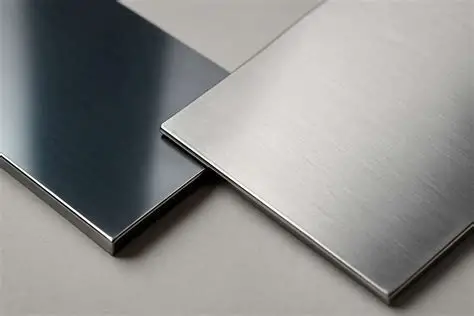
Comprehensive Comparison Table
| Property / Machining Factor | 1018 (Low-Carbon Steel) | 4140 (Alloy Steel, Pre-Hardened ~28–32 HRC) | 303 (Free-Machining Stainless) | 304 (Austenitic Stainless) | 316 (Austenitic Stainless, Mo) | 17-4 PH (H1025/H1150) |
| Tensile Strength (typical) | ~440 MPa | ~850–1000 MPa | ~620 MPa | ~515–620 MPa | ~515–620 MPa | ~930–1100 MPa |
| Hardness (typical) | ~120–160 HB | ~28–32 HRC | ~160–200 HB | ~150–200 HB | ~150–200 HB | ~28–38 HRC |
| Machinability Rating (vs. B1112 = 100%) | ~70% | ~55–65% | ~75% | ~40% | ~36% | ~40–45% |
| Typical Turning Speed, Carbide (SFM) | 400–700 | 300–500 | 300–450 | 200–350 | 150–300 | 150–300 |
| Work-Hardening Tendency | Low | Low–Moderate | Moderate | High | High | Moderate |
| Thermal Conductivity (W/m·K) | ~51 | ~42 | ~16 | ~16 | ~15 | ~18 |
| Relative Tool Life | Baseline (best) | Good | Good | Moderate–Short | Short | Moderate |
| Typical Achievable Tolerance | ±0.01–0.025 mm | ±0.01–0.025 mm | ±0.01–0.025 mm | ±0.02–0.05 mm | ±0.02–0.05 mm | ±0.01–0.025 mm |
| Typical Ra After Machining | 0.8–1.6 µm | 0.8–1.6 µm | 0.8–1.6 µm | 1.6–3.2 µm (finer with tuned finishing) | 1.6–3.2 µm | 0.8–1.6 µm |
| Corrosion Resistance | Poor (needs plating/coating) | Poor (needs coating) | Good | Very good | Excellent (chlorides, marine) | Good |
| Relative Machining Cost | Low | Low–Medium | Medium | Medium–High | High | High |
General tolerance classes such as ISO 2768-m (medium) are achievable on both families in standard operations. Tighter tolerances (IT6–IT7 and below) are achievable on both, but stainless typically needs more finishing passes and stricter process control to hold them.
Key Differences in CNC Machining
Machinability & Cutting Speeds
Carbon steels like 1018 and 1045 cut predictably. Chips form and break cleanly, cutting forces are moderate, and the process window for speed and feed is wide. Most shops run carbide inserts at high surface speeds with standard flood coolant.
Austenitic stainless grades (304, 316) behave differently for three reasons:
- Work hardening. The surface layer hardens when the tool rubs instead of cutting. A dwell, a dull edge, or too light a finishing pass produces a hardened skin that damages the next pass. Stainless needs positive feeds and a tool that keeps cutting.
- Gummy chip formation. Long, stringy chips tend to wrap around the tool and workpiece. They raise cycle time through chip-clearing cycles and can scratch finished surfaces.
- High cutting forces. Stainless requires rigid setups and lower surface speeds. 316 is typically slower again than 304 because of molybdenum content.
In practice, expect 304 and 316 to run at roughly half to two-thirds of the surface speed you would use on 1018 or 1045. Cycle time on stainless parts increases accordingly.
Free-machining grades like 303 (sulfur-modified) close part of this gap, with better chip breaking and a lower tendency to build up on the tool. The tradeoff is slightly reduced corrosion resistance and weldability compared with 304, which matters for food, marine, or welded assemblies.
Tooling & Wear
Tool cost is one of the largest hidden differences between the two families.
Carbon and alloy steel: Standard coated carbide inserts (TiN, TiCN, TiAlN) give long, predictable tool life. Roughing and finishing can often share insert families. At 28–32 HRC, 4140 is tougher on tools than 1018 but still within a normal tooling budget.
Stainless steel:
- Sharp, positive-rake geometries reduce rubbing and work hardening.
- Coatings tuned for heat resistance (TiAlN, AlCrN) extend tool life at the elevated temperatures stainless creates.
- Built-up edge (BUE) is a recurring problem on 304 and 316. It degrades surface finish and causes unpredictable dimensional drift over a production run.
- Notch wear at the depth-of-cut line is common, and inserts are often indexed or replaced earlier than on carbon steel to protect tolerance.
- Drilling and tapping are especially sensitive. Dull drills harden the hole wall, and taps break more often in 316 than in 1018. Thread milling is often preferred over tapping for critical stainless threads.
For production runs, this affects the cost model in two ways: more frequent insert changes and more tool-offset adjustments or in-process probing to maintain size.
Thermal Management & Distortion
Thermal conductivity is the physical root of many differences between the two families. Carbon steel conducts roughly three times more heat than austenitic stainless (about 51 vs. 16 W/m·K). In stainless, less heat leaves through the chip and workpiece, so more stays at the tool edge.
Consequences:
- Tool temperature rises faster, accelerating crater and flank wear.
- Local workpiece heating causes thermal growth during the cut. Thin walls, long slender shafts, and large flat surfaces are most vulnerable.
- Thermal expansion is higher in austenitic stainless (roughly 16–17 µm/m·°C vs. about 11–12 for carbon steel), which compounds dimensional drift when tolerances are tight.
Mitigation on stainless typically includes high-pressure or through-tool coolant, consistent coolant concentration, rough-then-finish strategies with stress-relief or cooling time between operations, and symmetrical material removal on thin-walled parts. For tight-tolerance stainless parts, measuring only after the part reaches stable temperature avoids false rejects.
Carbon steels still require attention to residual stress, especially in heavily machined bar or plate stock, but they are generally more forgiving.
Tolerances & Surface Finish
Both families can hold tight tolerances, but the effort differs.
- Carbon steel: Stable cutting conditions make ±0.01 mm achievable on turned and milled features with standard process control. Surface finish of Ra 0.8–1.6 µm is routine, and finer finishes are straightforward with grinding or honing.
- Austenitic stainless: Tolerances of ±0.02–0.05 mm are typical for standard production, and tighter requirements usually need dedicated finishing passes, sharper tooling, and in-process verification. Ra 1.6 µm is a normal as-machined target. Reaching Ra 0.8 µm or finer is possible but typically involves tuned feeds, fresh inserts, or a secondary operation.
- 17-4 PH and martensitic grades (410, 420, 440C): These hold tolerance and finish more like alloy steel and can be machined in the solution-annealed condition, then aged for final strength. Because aging causes small dimensional changes, drawings with tight tolerances should be machined with this shift planned for.
Surface finish also interacts with corrosion performance. Smeared or heat-tinted stainless surfaces can reduce corrosion resistance. Passivation (per ASTM A967 or equivalent) is commonly specified after machining to restore the passive layer. Carbon and alloy steel parts typically need protection through zinc plating, black oxide, nickel plating, or paint, with the plating thickness factored into final tolerance.
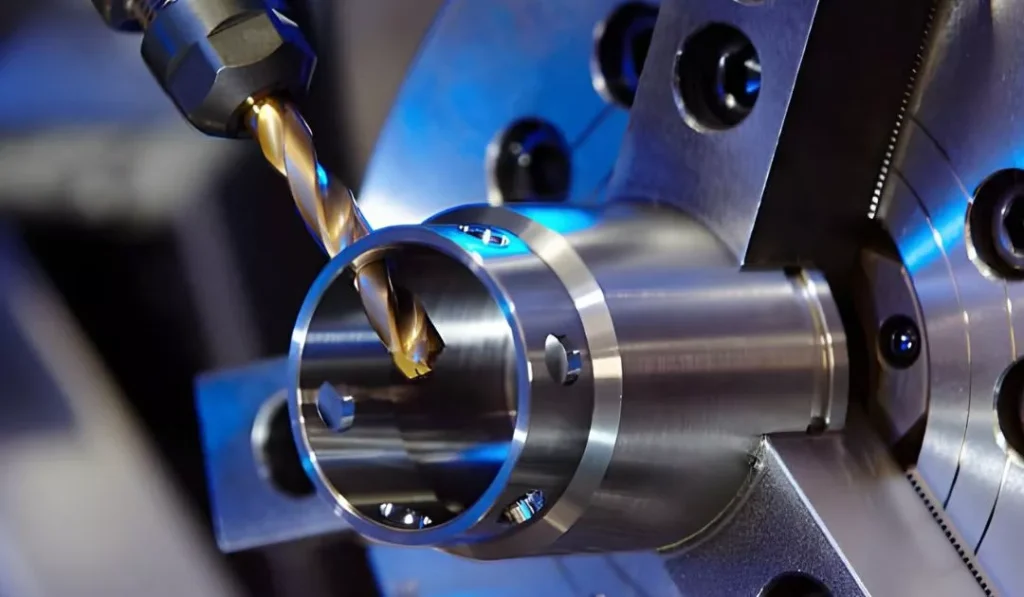
Cost Comparison
Comparing raw bar prices alone misleads. For machined parts, material cost and machining cost often move in opposite directions in importance.
Raw material cost: Stainless bar typically costs more per kilogram than 1018 or 1045, and 316 costs more than 304 because of nickel and molybdenum content. Pricing varies with alloy surcharges and market conditions, so quote against current supplier data rather than fixed assumptions.
Machining time: Lower surface speeds and more finishing passes mean longer cycle times per part on stainless. For small and mid-size parts, this often outweighs the raw material difference.
Tooling cost: More frequent insert changes and higher-grade coatings add per-part cost on stainless.
Setup and fixturing: Thin-walled or tight-tolerance stainless parts may need softer jaws, support fixtures, or multi-stage machining to control distortion. This adds setup time, especially in low-volume orders where it is spread over fewer parts.
Secondary operations: Carbon steel almost always needs a protective finish (plating, black oxide, or coating). Stainless often needs only passivation, which can narrow the total finished-part gap, particularly when plating adds cost and lead time.
Rule of thumb for DFM: For parts that would be plated anyway, compare the total cost of carbon steel plus finishing against stainless plus passivation. For small, complex parts in 316, machining time frequently dominates the price. For large, simple parts, raw material weight becomes a larger share.
Cost-saving options on stainless:
- Specify 303 instead of 304 when corrosion exposure is moderate and welding is not required.
- Relax tolerances and finish callouts on non-functional surfaces.
- Avoid deep, narrow pockets and thin walls where possible.
- Use standard hole sizes and thread specs to match available tooling.
- Consider 416 or 17-4 PH where hardness or strength matters more than maximum corrosion resistance.
Application Scenarios
When to Choose Carbon or Alloy Steel
- Structural and load-bearing components: shafts, gears, spindles, couplings, and fixtures where strength and cost matter most.
- Indoor or controlled environments: parts that will be oiled, coated, or plated and will not see wet or chemical exposure.
- High-volume cost-sensitive production: where cycle time and tool life drive unit price.
- Heat-treated wear parts: 4140 or 4340 hardened and tempered to a specified HRC for strength and fatigue resistance.
- Tooling, jigs, and fixtures: where machinability and dimensional stability matter more than corrosion resistance.
When to Choose Stainless Steel
- Corrosive or washdown environments: food and beverage equipment, pharmaceutical processing, and marine hardware.
- Medical and laboratory components: 316 or 316L for cleanability and corrosion resistance.
- Exposure to chlorides or chemicals: 316 over 304 where pitting resistance is required.
- Parts where plating is undesirable: designs that cannot tolerate flaking, contamination, or coating wear.
- High-strength with corrosion resistance: 17-4 PH for aerospace fittings, valve components, and pump shafts.
- Visible components: where appearance and long-term surface stability matter.
Conclusion
Carbon and alloy steels machine faster, wear tools less, hold size more easily, and cost less to cut. Stainless steels cost more to machine because of work hardening, low thermal conductivity, and tool wear, but they can eliminate plating, reduce lifecycle maintenance, and survive environments where carbon steel cannot. The right choice depends on the service environment, tolerance requirements, volume, and total finished-part cost, not on bar price alone.
At Xtmade, our engineering team machines both material families daily across CNC milling, turning, and multi-axis work. If you are unsure between 1045 and 304, or between 304 and 316 for a specific part, we can review the geometry, tolerances, and surface requirements and recommend the lowest-cost grade that meets your functional needs.
Upload your CAD files (STEP, IGES, or PDF drawings) to receive a free DFM review and RFQ quote. Our engineers will flag features that drive up machining time, suggest grade or tolerance adjustments, and provide a detailed quote with lead time. Submit your files through the Xtmade quote page to get started.

